inquiry
Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit
Home

die casting part grinding robot

die casting part grinding robot

  • Grinding Robot Rigidity, Payload and Heavy Gate Cutting: Three Specs Foundries Usually Misread
    Nov 01, 2026
    Grinding Robot Rigidity, Payload and Heavy Gate Cutting: Three Specs Foundries Usually Misread   When a foundry compares grinding cells, the first glance is almost always the same: how many axes, what envelope, what rated payload. Those numbers sit neatly in a brochure. What shows up after start-up is different. The wheel chatters on a gate stub, the spindle bogs, the path drifts a fraction, and everyone argues about the program. Iron and steel make this obvious. Aluminum flash is thin; you buy speed and a sharp cutter. Iron and steel gates, risers and parting-line fins — especially stubs that still carry scale before heat treat — buy rigidity and sustained cutting force. Three numbers that share a spec sheet are not the same thing on the floor. Rated payload, table capacity and cutting force A 200 kg arm rating does not mean the machine can push a wheel with 200 kg of force. Payload is how much the arm can carry: spindle, dressing, gripper. Table capacity is fixture plus casting. Cutting force is what the wheel can keep on the stub without the path floating. A general-purpose six-axis with a spindle hung on the flange often has little payload left. Ask it to chew a thick gate and the gearbox and arm give first. The programmed path still runs. The actual depth of cut does not. Operators call it “inaccurate teaching.” The structure is yielding. NEVIEW states this without dressing it up on the iron DR line. On the DR-750B, table and arm are both in the 200 kg class. On heavy gate stubs, sensor trials have seen more than 165 kg of acting force. That figure is not a slogan. It says the load during stub cutting is real and it lands on the machine and the fixture. Selecting only because “the casting weighs less than 200 kg” usually means extra passes later, and the cycle time falls apart. Why heavy gates punish a soft structure Flash on a flat face is polite. Contact area is predictable. A gate stub is not. The section is ragged, sometimes with shrinkage or burnt-on sand. The instant the wheel bites, contact jumps and the force spikes. A skilled grinder eases off, changes angle, takes two or three bites. A robot that keeps a fixed normal force on a soft machine shows three familiar faults: chatter that kills wheels; path give that leaves a ring at the root; fixture creep that throws every later hole and parting line off. On heavy iron, the first question is not “can we teach it.” It is “can this structure take the force at the stub.” Dual stations, enclosures and vision matter. They come after the force path is closed. Material changes the demand High-volume iron with reasonably regular gates fits a rigid dual-station DR cell: DR-550B for smaller parts, DR-750B for mid-size, DR-950B and DR-1200R/B when envelope and mass climb. Cut first, then argue takt. Steel is harder on the same stub. GR-750B and GR-950B raise spindle power and capacity for a reason. Wheel cost on steel already hurts; add chatter and the consumable bill outruns depreciation. Aluminum is a different job. You rarely lean on a stub with that kind of force. You trim flash, gate roots and cavity corners. The MR line is about cutter speed and compliant contact. Thin walls dent if you shove. You still need stiffness — to hold the path, not to ram the part. Giga-castings are a third case. Once the envelope approaches something like φ2300 mm, the problem is stiffness at long reach. The same tip force becomes a much larger moment at the base. Those cells are not catalogue machines. Floor space, number of spindles, floating versus rigid heads are all part-specific. Spindle kilowatts are not cutting capacity Motor power is one link. Holder stiffness, wheel diameter, surface speed, feed and whether the fixture backs the cut all sit in between. Oversized wheels raise surface speed and also the overhang. Undersized wheels cut but eat changeovers. Iron wants wheels and burrs; aluminum wants mills and disc cutters. Swap the logic and you load the cutter or cut through a wall. Compensation is separate. Stub height varies with the casting. Without a probe or displacement check, a rigid machine only repeats the same wrong depth. Path correction from measured offset, and current/position/torque loops for parts that flex, solve different shop problems. Do not mash them into one phrase. Why a converted general-purpose arm struggles on thick stubs A stock robot, an electric spindle and a spark shield quote well and ship fast. Shallow aluminum flash in small batches can live with that. Mid-to-large iron with continuous stub cutting runs out of structural margin first. A foundry-built cell sizes table, arm, spindle and enclosure for the same force path. The dual-station table has to hold during the cut. The cabin has to live with dust and vibration, not only hide sparks. Skip that and the machine will run on day one. Three months later you watch gearbox temperature, repeatability and wheel spend. Not every plant needs the heaviest frame. Small, regular iron with gates already sawn back can live on a DR-550B envelope. Buying a DR-1200 “for later” drags floor space, power and fixture cost with it. Rigidity should be enough. Bigger is not automatically better. What to ask and what to try Try the worst stub, not the pretty face. Ask whether rated payload includes the spindle and the toolholder. Check that the fixture supports the cut direction so the part is not lifted. Run a dozen pieces and watch whether root stock grows. Heat, wheel wear and micro-shift stack up; a single try-out hides them. On steel, watch wheel spend. If the machine is quiet, consumables become a number you can plan. If changeover is frequent, budget fixtures and vision on their own line. Do not hide that cost inside “cutting capacity.” Close Whether a grinding robot holds up in a foundry fettling bay is not decided by axis count on a slide. It is decided at the gate stub — hard, irregular, unforgiving. Get rigidity, payload and cutting force straight. Dual stations, sealing and compensation are worth discussing after that. If those three are wrong, editing the program will not stiffen the machine.
    Read More
  • On mixed-SKU casting grinding, changeover time is rarely the robot program
    Oct 15, 2026
    On mixed-SKU casting grinding, changeover time is rarely the robot program Many foundries size a grinding cell on one representative part. Three months after start-up, output is eaten by two-hour changeovers — and by the half-shift of hand touch-up that follows. A single-part cycle chart often dies on a mixed line Quotes for automated grinding are almost always built on one part: flash length, gate stub size, minutes per cycle, whether dual stations overlap load and grind. The spreadsheet looks clean. The shop floor runs a different clock. Valve bodies in the morning, brackets after lunch, two pallets of housings squeezed in the next day. The representative cycle time is still true. What is not true is dividing 480 minutes by that number. Subtract fixture swap, tool swap, probing, first-article grind, and quality release. That remainder is the real shift. People call this “slow program change.” Calling a program on the HMI takes seconds. Locating the part, matching the tool, keeping the compensation datum, and getting first-article sign-off are slower. Three of those four have little to do with the robot brand. Changeover is four layers, not one motion Shops treat changeover as stop, swap, run. It is at least four layers. Program: path, spindle speed, feed, force or compensation settings. This layer is fast if programs live under a part number, not in someone’s teach-pendant backup. Fixture: clamps, locators, jaws, or a complete tooling plate. Casting sand wears pins. A hole that matched the drawing in month one does not match in month six. Tool: wheels, burrs, mills, flap wheels are not universal. A hard wheel sized for iron gate stubs will tear an aluminum skin. An aluminum face mill on ductile-iron flash goes dull in minutes. A tool change usually needs balance or a touch-off. Skip that and the first pass vibrates the new path off. Datum: probe points, vision templates, safe retracts. Points that sat on a valve body last week may land on flash or empty air on this week’s bracket. A wrong probe point is worse than no compensation. If any layer is unprepared, a “15-minute changeover” on the form becomes an hour. Many acceptances run eight hours on one SKU. Changeover is never in the scorecard. Fixtures are where most plants actually lose the hour Stable families can live with a self-clamping fixture or a press-down unit and only swap locators. Plants with scattered geometries are different. A valve uses a register, a bracket uses two pads, a housing sits on the cavity. A “universal fixture” usually locates universally badly. Simple pins are cheap and quick to change. They are also sloppy once parting-line shift shows up. Hole-break edges then vary lot to lot, machining sends parts back, and the simple fixture grows extra stops until it is no longer simple. Self-clamping tooling locates well and behaves like a small machine of its own when you swap it. Lead time is long, storage is real, and door-swing interference on a three-station table often appears only at install. AI grinding’s honest benefit on changeover is fewer hard locators. A tray or a coarse stop can be enough for the vision system to find pose. That does not turn a thin aluminum housing into a rigid body. Vision finds the part. Cutting force and chatter still need support. When tools lock you to a material family, changeover becomes a cell change Iron cells are built around wheel load and stub cutting. Aluminum cells more often run face mills, cutters, or belts. Steel adds hardness. Hanging an iron wheel and an aluminum mill on one spindle is possible on paper. Dust mix, filter fire risk, hood opening, and airflow are designed around one chip type. Few plants keep that mix for long. Mixed SKUs therefore does not mean one cabin for every alloy. The cheaper split is usually iron on one cell, aluminum on another, then size bands inside each family. Changeover stays inside a family where fixtures and tools still share something. Forcing a ductile valve and an aluminum housing through the same cabin puts spindle maps, dust mode, guarding, and base plates on the changeover list. The machine you saved is paid back in lost hours and process risk. A stored program and a re-taught program are two different factories Someone who can teach a robot is not the same as someone who owns a program library. Names like “valve2”, “valve2-fix”, “final” mean nobody will call the file three months later. Changeover becomes: open the nearest path and re-touch the critical points. Compensation belongs with the part number: probe coordinates, allowable offset, force cap. Store only the path and the probes stay where the last product left them. First article either cuts into parent metal or leaves a ring of flash. A Chinese teach pendant shortens training. It does not replace version control, first-article records, or a name on the last path edit. When the senior operator is off, that gap hurts more than a spindle alarm. Vision shortens finding the part. It does not skip process prove-out High mix, modest volume is the usual reason to look at AI grinding. You weld fewer hard fixtures. For housings and brackets that do not justify a full clamp set, that reason holds. What does not hold is the hope that vision makes changeover a start button. The template says which product this is. It does not say how tall this gate stub grew after a tooling wear week. Tool strategy and compensation still sit per family. A new part still needs a first article and a feed tweak. Treat AI as “no process work” and you will rework. It cuts fixture count and search time. The process window stays. On tight windows, first-article time after a change can exceed the fixture swap itself. Not every high-mix shop should chase one cell for the whole list Mixing on one cell usually needs several conditions at once: same material family, size inside one table, similar burr shape so tools can be shared, enough daily volume to keep changeover count tolerable, and a shop willing to keep fixture and program books. Bad mixes are equally concrete: iron with aluminum, stub cutting with cosmetic faces, prototypes stealing a production cell, downstream machining that already uses the ground edge as a datum. A second cell looks expensive until you add changeover, touch-up, and scrap. A middle path is common: one cell locked on two similar runners that make most of the tons, a third geometry left to a bench or a vendor. Automation does not have to cover every drawing number. Covering the two numbers that are 80% of output is often the better buy. If the changeover sheet is vague, cell speed does not matter On the machine side: dual stations so the door is not the cycle, HMI recall by part number, fixture quick-change interfaces, at least a quick-change tool flange, compensation stored with the program. Dedicated foundry cabins tend to hold these together because table, door, and dust are designed as one cycle. A general-purpose robot in a fence usually does not. The plant owns the other half. Fixtures wiped before the swap, pins replaced on a calendar, wheel remaining diameter written down, first-article dimensions listed, a rule for whether a bad part means a path edit or a locator check. Without that sheet, a twenty-minute vendor changeover still dies in the afternoon. Scheduling has to change with it. Three unrelated geometries in one shift will beat any spindle. Run a family together. Park changeovers at shift start. “Cut over any time” is a sentence from a presentation, not from a grinding bay. Ask how many times a day you change before you ask if the robot can grind Whether a grinding robot can physically cut a casting is the first sourcing question. On a mixed line it is not the deciding one. The deciding questions are whether those drawing numbers belong in one cabin, and which of the four changeover layers you have actually prepared. A program that appears on the screen only proves the integrator shipped a file. Repeatable location in twenty minutes, tools that stay inside one material family, probe points that travel with the SKU, and a signed first article — that is changeover capability. Miss one, and you are back to the single-part chart that never described the shift.
    Read More
  • Foundries Can’t Keep Grinders. What Work Can a Grinding Robot Actually Take?
    Foundries Can’t Keep Grinders. What Work Can a Grinding Robot Actually Take?
    Sep 10, 2026
    Foundries Can’t Keep Grinders. What Work Can a Grinding Robot Actually Take?     The hardest shift to staff in a foundry is often not melting or molding. It is grinding. Day shift can still be patched together. Night shift, hot weather, and year-end rush orders are when the finishing room empties first. The work is not optional. Unground gates, proud parting lines, and hole-edge burrs show up later in machining, assembly, and paint. The job is dirty, loud, and dusty. Numb hands and sore wrists are normal. When a skilled grinder leaves, you do not replace the “feel” in a week. Most plants looking at grinding robots are not chasing a slogan. They are asking a simpler question: can this line still ship tomorrow. What actually wears people out From outside, grinding looks like an angle grinder on a casting. Anyone who has stood in the booth knows fatigue is only part of it. The harder problem is inconsistency. Castings from the same mold and the same heat do not arrive the same. Gate stubs vary in height. Flash is thick on one piece and thin on the next. Some parts are slightly warped. Some cavities will not accept a wheel. A skilled operator compensates by pressure, angle, and a couple of extra passes. A new hire under-grinds or knocks a datum face down. Piecework continues. Quality starts to drift. Turnover makes it worse. Training a finisher takes time. Losing one experienced person takes cycle time and rework with them. Job ads can stay online. Castings will not wait. Dust and labor rules are also pushing the job out of the plant. Iron dust, aluminum smear and noise, steel cutting load—none of that is solved by handing out earplugs. “Just hire two more people” is getting harder to use as a finishing strategy. That is why automated grinding is entering foundries. Finishing has started to hold the whole line back. Why casting grind is more awkward than machining Machining starts from a blank that already has datums and tighter stock. Casting grind starts from something else. Gate remnants can be high. Cutting force jumps immediately. Parting lines, vents, cold-shut edges, and ingates are irregular. The tool has to reach in without thinning the wall next to it. Sand castings and permanent-mold parts, iron and die-cast aluminum, do not leave the same burr. Die-cast flash can be thin and long. A sand-cast gate can be thick and hard. Then there is casting variation. A millimeter or two on the same part number is not rare. A robot that only repeats one frozen path will grind air one day and cut into a rib the next. That is why a demo video can look clean and the same cell can disappoint on a real floor. Demo parts are usually better behaved than incoming work. The hard part is not whether the arm can move. It is whether three things can hold at once: the part can be located with acceptable repeatability; the path can move with the casting error; tooling and force can change by material and by feature. Miss one, and the cell still runs. The quality does not. What a robot can take—and what it should not Start with the good fit. Stable volume, a short list of part numbers, and a grinding spec you can write down. Housings, brackets, valve bodies, wheel-type parts where the same gates, the same flash lines, and the same hole edges come back every day. That repetition is what a cell is built for. Dual stations exist for a practical reason: grind on one side, load on the other, so the machine is not waiting. For mid-volume small and medium iron or aluminum parts, that layout matches finishing better than a single fixture and a standing robot. Heavy gates and thick flash are where people fade. Handheld tools lose force late in a shift and the cut goes uneven. A rigid, high-payload grinding unit is often steadier there. What matters on site is whether the table and arm can take the cutting force, and whether the enclosure actually contains dust and sparks—not how the machine photographs. Now the poor first candidates. Job shops with constant part-number changes will burn time on fixtures and teaching. If the casting may be revised before the clamp is finished, the cell becomes furniture. That is not “automation is impossible.” It means changeover rate and who owns the program have to be answered first. Parts with almost no stable datum, or with very large piece-to-piece spread, also need caution. A dead path without measurement and compensation can create more rework than a person. Distortion-prone parts—thin aluminum walls, some covers—need force control, not more stiffness. If the machine cannot go light where it must go light, cosmetic faces ripple. One more miss: grinding is only one slice of finishing. If cutting and shot blast are unstable, and sorting and transfer are still a crowd of people, one grinding booth just moves the bottleneck a meter downstream. Iron, aluminum, steel, and mega die cast are not the same job Cast iron: hard gates, heavy dust, fast wheel wear. The unit has to hold load, and dust collection cannot be decorative. Once iron volume is there, dual stations and dual spindles show up because waiting time is expensive. Aluminum is different. It smears. Surfaces mark easily. Many aluminum jobs need flash gone and edges even, without wounding a datum. Tools change: disc cutters, mills, belts, brushes. An iron-grinding wheel strategy does not transfer. Thin walls need fine current, position, and torque loops. If those loops are crude, appearance parts show waves. Steel asks for rigidity. The same gate size cuts harder than iron. If payload and table capacity are short, a pretty path still chatters. Large integrated die-castings are another project type. Big envelopes, long flash, many surfaces, and a takt set by the die-cast cell. Scaling a standard booth is not the work. Floor space, handoff from the casting island, and fixture strategy decide the project. You do not buy “a robot.” You buy a finishing method for a material, a geometry, a volume, and a process. What plants usually underestimate Fixtures. Simple nests are fast and cheap, and they move. Self-clamping nests are stable and slow to build. Some machines add a press-down axis to drop some cylinder modules and cover more part numbers. “The robot has a camera, just dump the parts” is still rare on real foundry floors. Vision and auto-locate, when they are used, are there to cut hard locators and cut reteaching—not to delete fixturing. Consumables and process. Wheels, burrs, discs, flap wheels, rotary files for iron and steel; a different set for aluminum. The wrong tool on the right machine still makes scrap. A cell does not arrive knowing which cutter belongs on which feature. Incoming consistency. Mold upkeep, pouring stability, and how the gate was cut before grind all land on the program. Compensation can swallow some size scatter. It cannot swallow a process that is not under control. Before automation, tighten gate location and flash condition. Do not ask the cell to eat every upstream swing. Ownership. Someone has to own programs, changeovers, wheel changes, and compensation values. A supplier cannot live in the plant forever. If nobody on the floor will touch the teach pendant, a good start-up decays in a few months. Four questions before you buy Will these part numbers still run in six months? Is there enough daily volume to feed a full shift? Can process engineering mark the gates, the flash, and the faces that must not be touched? Is there a person who will own fixtures and programs? If two of those are blank, do not start with “lights-out.” Start with the dirtiest, heaviest, most repetitive features. Lock takt and quality. Then decide whether bin picking, infeed conveyors, or sorting belong in the next step. For foundries and die-casters that already have stable volume, the value is usually plain: quality that does not collapse when a skilled grinder quits; finishing that can still run on night shift; fewer dust and labor fights; the same part number finished to the same standard, regardless of who is on the wheel that day. Companies that live in casting finishing—Neview is one of them—are judged on whether compensation tracks casting scatter, whether a heavy gate can be cut, whether aluminum can be worked lightly, whether iron and steel can be held, and whether the grind cell can connect to handling later. Those points only mean something against a real part and a real volume. Automated grinding will not clean up an entire foundry. It is good at the work that repeats every day, can be specified, and has already worn people down. The shop-floor test is still the same: when the skilled hand is gone, does the part still come out the same.  
    Read More
  • Beyond Manual Grinding: How NEVIEW Casting Grinding Robots Are Solving the Foundry Labor Crisis
    Beyond Manual Grinding: How NEVIEW Casting Grinding Robots Are Solving the Foundry Labor Crisis
    Aug 08, 2026
    Beyond Manual Grinding: How NEVIEW Casting Grinding Robots Are Solving the Foundry Labor Crisis   Walk into any foundry today, and you’ll likely hear the same pain point: it’s getting harder and harder to find skilled grinding operators. The work is physically demanding, noisy, dusty, and potentially hazardous. Young workers are increasingly unwilling to take on these roles, and the aging workforce means decades of expertise are retiring from the shop floor. For foundries around the world, this isn’t just an HR problem—it’s an existential challenge. NEVIEW provides the answer with advanced casting grinding robots built specifically to handle the harsh realities of post-casting finishing. The True Cost of Manual Grinding Manual grinding appears cheaper at first glance, but hidden costs accumulate fast. Inconsistent pressure leads to over-grinding, scrap parts, and rework. Operators tire, causing cycle-time variations and quality dips during late shifts. There’s also the rising expense of personal protective equipment, ventilation upgrades, and work-related injury claims. When you calculate total cost per acceptable part, manual processes often prove far more expensive than automation. Enter the NEVIEW Casting Grinding Robot NEVIEW casting grinding robots are engineered from the ground up to tackle iron, steel, and aluminum castings of varying complexity. Equipped with high-torque spindles, force-sensing compliance, and intelligent path planning, these robots remove gates, parting lines, and flash with precision that manual operators struggle to match consistently. The enclosed work cell contains dust and noise, transforming a dirty, dangerous corner of the foundry into a clean, monitored, and predictable operation. How Force Control Changes the Game A key differentiator for NEVIEW robotic grinding systems is real-time force feedback. Unlike rigid CNC machines or basic robotic position control, NEVIEW robots feel the part. The end effector maintains a constant contact force against contoured surfaces, automatically compensating for part-to-part dimensional variation—a common reality in sand casting. This adaptive capability means fewer scrapped castings and more uniform output, even as tooling wears or mold shifts occur between batches. Seamless Integration, Not an Island Modern foundries don’t need a standalone robot that creates a bottleneck. NEVIEW designs its grinding cells for easy integration with existing shakeout, shot blasting, and machining lines. The vision system can recognize different part models, call up the correct grinding program, and process mixed batches without operator intervention. This flexibility is essential for jobbing foundries that handle diverse, small-to-medium production runs. Searches like “flexible casting grinding automation” and “NEVIEW foundry robot” naturally bring foundry engineers to content that addresses exactly these challenges. Building Workforce Resilience Far from “stealing jobs,” NEVIEW grinding robots let manufacturers redeploy their best people to higher-value tasks: quality inspection, process optimization, and running multiple cells. Companies that automate grinding report improved employee retention because they can offer upskilling programs rather than condemning workers to a lifetime behind a grinding wheel. This message resonates in recruitment and corporate branding, adding an indirect but powerful SEO and PR benefit. Conclusion The labor shortage in foundries isn’t a temporary trend—it’s a structural shift. Foundries that act now to adopt NEVIEW casting grinding robots will build a competitive moat: consistent quality, controlled costs, and a workforce focused on growth, not just survival. Explore the full range of NEVIEW automated grinding solutions and future-proof your finishing room today.  
    Read More
  • The Era of Green Foundries: How Grinding Robots Cut Energy & Consumable Costs
    The Era of Green Foundries: How Grinding Robots Cut Energy & Consumable Costs
    Jul 22, 2026
    How Grinding Robots Cut Energy & Consumable Costs Against the backdrop of global carbon neutrality and green manufacturing, foundries must balance high output with lower energy consumption and environmental sustainability. Post-casting grinding—traditionally a major source of energy use and consumable waste—is undergoing a green transformation through robotic automation. 1. Optimizing Grinding Paths to Extend Abrasive & Tool Life In manual grinding, uneven force often leads to premature wheel wear or tool breakage. Grinding robots utilize constant force and surface speed control to wear abrasives down evenly, boosting tool life by over 30% and directly trimming consumable budgets. 2. Cutting Factory Energy Consumption & Dust Collection Load Unlike traditional open-shop dust extraction, robotic grinding workstations feature enclosed dust containment enclosures. Paired with localized suction systems, they trap particulates at the source while cutting power usage for facility-wide HVAC systems. 3. Enhancing Workplace Health to Pass Global ESG Audits Global buyers—such as automotive OEMs and heavy machinery leaders—increasingly weigh EHS and ESG (Environmental, Social, and Governance) standards during supplier audits. Implementing grinding robots cleans up the shop floor, lowers occupational safety risks, and cuts waste, giving foundries a distinct edge in securing high-value international contracts.
    Read More
  • Conquering the Toughest Foundry Challenge: Why Automated Grinding is the Future
    Conquering the Toughest Foundry Challenge: Why Automated Grinding is the Future
    Jul 07, 2026
     Conquering the Toughest Foundry Challenge: Why Automated Grinding is the Future   In the modern foundry supply chain, the cleaning and finishing shop has long been considered the ultimate bottleneck of the entire facility's production capacity. Traditional casting deburring, cleaning, and grinding processes rely heavily on intensive manual labor. This conventional approach not only saddles factories with heavy management costs but also exposes fatal weaknesses in fierce global competition. The harsh environments characterized by high dust, high noise, and high vibrations drive younger workers away, making recruitment difficulties and high turnover rates an ongoing norm. Meanwhile, manual grinding is highly susceptible to physical fatigue and emotional variance, resulting in poor product consistency and stubbornly high scrap rates. With the seamless advancement of global Industry 4.0 and smart manufacturing, grinding robots are becoming the standard weapon for leading foundries worldwide to break this deadlock. Compared to traditional manual labor, automated grinding systems offer unparalleled long-term strategic advantages:   Ultimate Surface Consistency and Quality Stability: With manual grinding, the pressure and angle applied in the 1st hour differ drastically from those in the 8th hour. Conversely, grinding robots operate strictly according to digitally preset trajectories and parameters, ensuring that the removal of flashes and burrs on every single casting achieves 100% identical quality, perfectly satisfying stringent quality inspection standards.   Significantly Enhanced Safety and Regulatory Compliance: The massive amount of metal dust released during grinding is a primary cause of pneumoconiosis, and severe vibrations cause chronic occupational diseases among workers. Transitioning workers from these high-risk environments into roles as robot operators and supervisors significantly mitigates corporate legal and medical risks while dramatically lowering employee turnover.   24/7 High-Efficiency Continuous Production with Shorter Lead Times: Robots do not experience fatigue, require sick leave, or suffer from shift-change lag; they can operate around the clock without interruption. When facing urgent orders from international clients, an automated grinding line can drastically compress delivery lead times, providing dependable delivery commitments. For foundries aiming to sustain long-term competitiveness in today's cutthroat market landscape, integrating casting grinding robots is no longer an optional choice—it is a critical matter of corporate survival. Facilities that embrace automation earlier will be the first to capture the dividends of high-end manufacturing.
    Read More
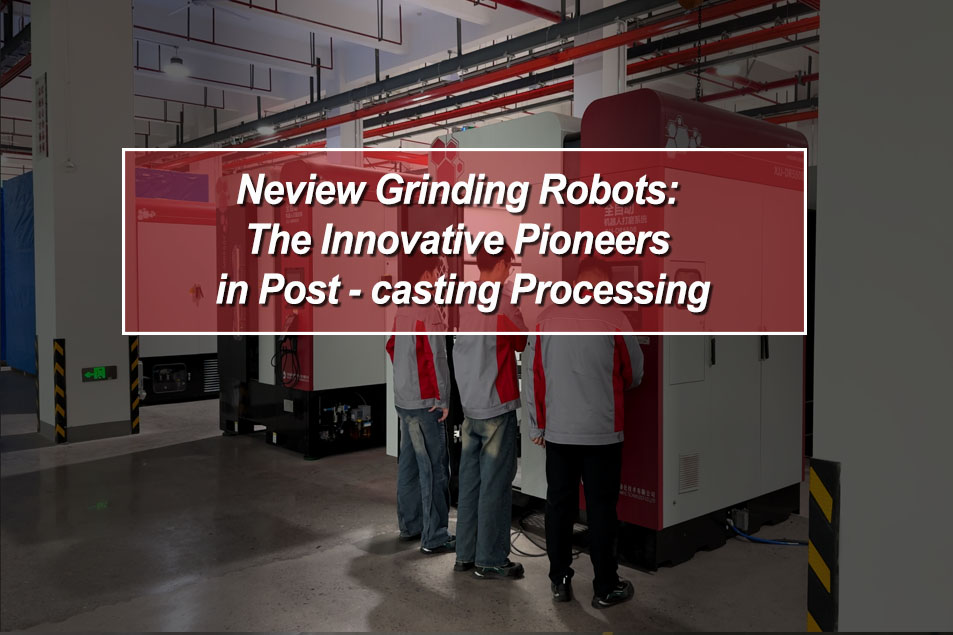
  • Neview Grinding Robots: The Innovative Pioneers in Post - casting Processing
    Neview Grinding Robots: The Innovative Pioneers in Post - casting Processing
    Jun 30, 2026
    Neview Grinding Robots: The Innovative Pioneers in Post - casting Processing Post - casting processing is a critical link in determining the final quality of castings. With its advanced technology and unique functions, Neview's grinding robots have become innovative pioneers in this field. The eight - axis seven - linkage structure of Neview's grinding robots endows them with unparalleled flexibility and adaptability. It can perform all - around and multi - angle grinding on the surface of castings, ensuring that every corner is finely processed. Whether it's a narrow gap or a complex contour, it can handle them with ease. This flexibility not only improves the grinding efficiency but also greatly enhances the grinding quality, making the casting surface smoother and more uniform, meeting the strict quality requirements of the high - end market. When dealing with different types of castings, Neview's grinding robots demonstrate strong adaptability. Whether they are small precision castings, such as the die - cast shells of electronic components, or large heavy - duty castings, such as the key components of construction machinery, it can precisely adjust the grinding parameters through the intelligent control system and advanced sensor technology to achieve the best grinding effect. For thin - walled castings that are prone to deformation, the robot can effectively remove burrs and defects without damaging the casting through the intelligent compensation and flexible fitting technology, ensuring the dimensional accuracy and surface quality of the casting. The automatic error detection and compensation system of Neview's grinding robots is another highlight. During the casting process, due to various factors, some dimensional and shape errors inevitably occur in the castings. This system can detect these errors in real - time and automatically adjust the grinding path to ensure that the grinding accuracy is not affected. This function greatly reduces the defective rate caused by casting errors, improves the consistency and reliability of products, and saves a large amount of cost and time for foundries. In addition, Neview's grinding robots are also equipped with an intelligent operation interface and remote monitoring function. Operators can easily set grinding parameters, monitor the running status of the robot, and carry out remote control through the intuitive interface. This not only improves the convenience of operation but also enables foundries to achieve intelligent management of the production process, promptly discover and solve problems, and further improve production efficiency and product quality.
    Read More
  • Neview Grinding Robots: The "All - Round Warriors" for Multi - Scenario Grinding
    Neview Grinding Robots: The "All - Round Warriors" for Multi - Scenario Grinding
    Jun 10, 2026
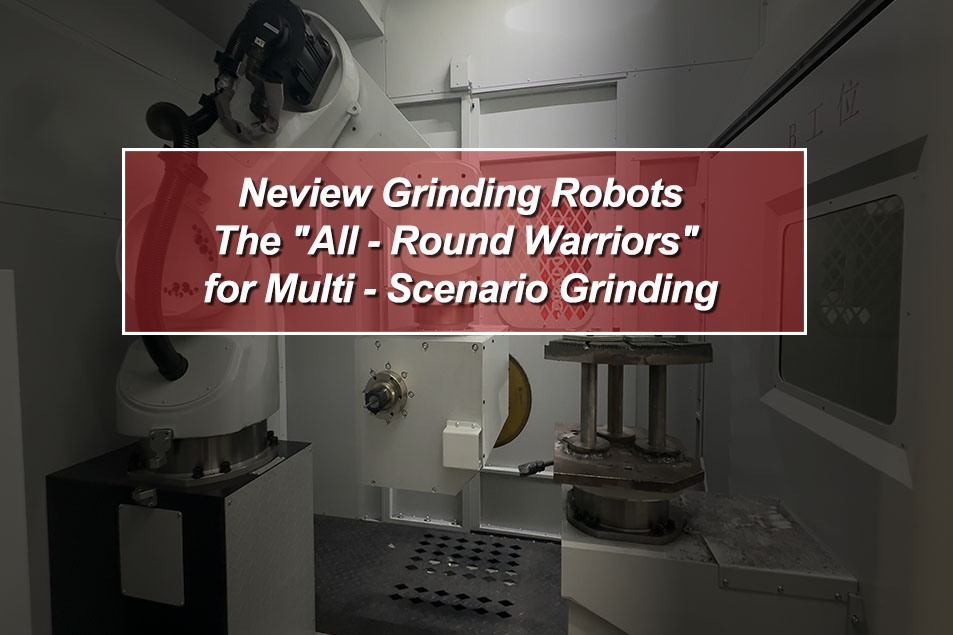
    Neview Grinding Robots: The "All - Round Warriors" for Multi - Scenario Grinding     In the foundry and related industries, the grinding scenarios are complex and diverse, posing extremely high requirements for the adaptability of grinding equipment. With its excellent performance and design, Neview grinding robots are like "all - round warriors", performing outstandingly in various grinding scenarios.     In the foundry workshop, grinding large - scale castings is an arduous task. The large load - bearing capacity of Neview grinding robots enables them to handle it easily. Taking the DR - 750B model as an example, both the workbench and the robotic arm can bear a 200 - kg - class load. When facing the thick riser stubs of large steel castings, it can stably apply sufficient grinding force to efficiently complete the cutting and grinding work, ensuring that the surface quality of large - scale castings meets high standards.     In the grinding scenario of small precision castings, accuracy becomes the key. Through the advanced control system and high - precision sensors, Neview grinding robots can precisely control the grinding force and position. In the post - die - casting grinding of electronic components, it can accurately remove tiny burrs without damaging the fine structure of the castings, meeting the strict requirements of small precision castings for high - precision grinding.     In addition, for castings with irregular surface shapes, the eight - axis seven - linkage structure of Neview grinding robots has demonstrated great advantages. This structure endows the robot with a high degree of flexibility, enabling it to flexibly adjust the grinding angle and path, closely fit the irregular surface for grinding, and ensure the uniformity and integrity of grinding. Whether it is a handicraft casting with unique curved surfaces or a mechanical part with a complex structure, it can be processed just right.     With its strong multi - scenario adaptability, Neview grinding robots provide comprehensive and reliable grinding solutions for different types of foundry enterprises, helping enterprises to efficiently produce high - quality products in various production scenarios.
    Read More
  • Neview Grinding Robots: The "Customization Masters" for Complex Casting Grinding
    Neview Grinding Robots: The "Customization Masters" for Complex Casting Grinding
    Jun 08, 2026
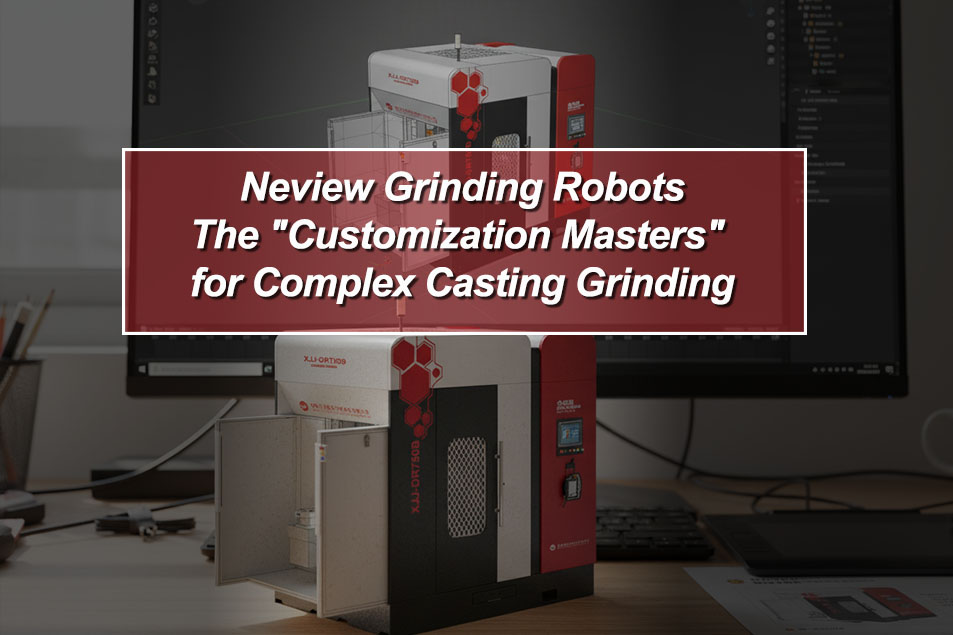
     Neview Grinding Robots: The "Customization Masters" for Complex Casting Grinding     In the foundry field, the diversity of castings poses numerous challenges to the grinding process. Neview grinding robots, with their remarkable customization capabilities, have become reliable assistants for complex casting grinding.     Neview grinding robots can adapt unique grinding parameters according to different casting materials, such as aluminum alloy, cast iron, and steel casting. Aluminum alloy is relatively soft and prone to deformation. The robot precisely controls the grinding force and speed to complete fine grinding without damaging the material. For high - hardness steel castings, the robot automatically adjusts the rotational speed and pressure of the grinding head to efficiently remove excess parts.     Complex geometric shapes also present difficulties in casting grinding. The eight - axis seven - linkage structure of Neview grinding robots endows them with extremely high flexibility. Whether dealing with castings featuring deep holes, thin - walls, or irregular curved surfaces, they can handle them with ease. For example, when processing aero - engine blades with complex curved surfaces, the multi - axis linkage of the robot can achieve all - around fitting, ensuring that every corner is ground thoroughly.     In addition, Neview grinding robots can be customized according to the production processes of foundries. From standalone operation to integration with other automated equipment to form an assembly line, it can seamlessly fit in. This high degree of customization enables Neview grinding robots to perfectly integrate into the production systems of foundries, significantly improving grinding quality and efficiency.
    Read More
  • Neview Grinding Robots: Leading the New Trend of Foundry Grinding Processes
    Neview Grinding Robots: Leading the New Trend of Foundry Grinding Processes
    May 18, 2026
    Neview Grinding Robots: Leading the New Trend of Foundry Grinding Processes   With the continuous advancement of technology, the grinding processes in foundries are undergoing profound changes. The Neview grinding robots, with their innovative technologies and excellent performance, have become the vanguard leading this trend of change.   Centered around its eight - axis seven - linkage structure, the Neview grinding robots achieve highly flexible and precise grinding operations. This unique structural design enables the robots to simulate the movements of human arms, conducting fine grinding on the surfaces of complex castings. Whether it is the delicate corners or complex curved surfaces, they can be processed just right. Compared with traditional grinding processes, it greatly improves the grinding coverage rate and uniformity, providing a strong guarantee for foundries to produce high - quality castings.   In terms of casting deburring, the Neview grinding robots show unique advantages. Their advanced intelligent control system can automatically adjust the grinding strategy according to the material, shape of the casting, and the distribution of burrs. Through the intelligent compensation and flexible fitting technology, the robots can efficiently remove burrs without damaging the castings, ensuring the flatness and smoothness of the casting surface. This intelligent deburring method not only improves work efficiency but also reduces potential quality problems that may occur during manual deburring.   The automatic error detection and compensation system of the Neview grinding robots is the key to maintaining high - precision grinding. During the casting process, due to various factors, there may be certain dimensional and shape errors in the castings. This system can detect these errors in real - time and automatically adjust the grinding path through precise algorithms, enabling the robots to adapt to the differences of different castings and always maintain stable grinding accuracy. This function effectively improves the consistency and reliability of products and reduces the defective rate.   In addition, the Neview grinding robots also focus on user experience and operational convenience. Its simple and intuitive operation interface enables operators to get started quickly, reducing training costs and operational errors. At the same time, the robots are equipped with remote monitoring and fault diagnosis functions, facilitating foundries to promptly understand the equipment operation status and carry out preventive maintenance to ensure the continuity of production.
    Read More
  • Unlocking the Potential of Grinding Robots: Neview Empowering Foundries
    Unlocking the Potential of Grinding Robots: Neview Empowering Foundries
    May 18, 2026
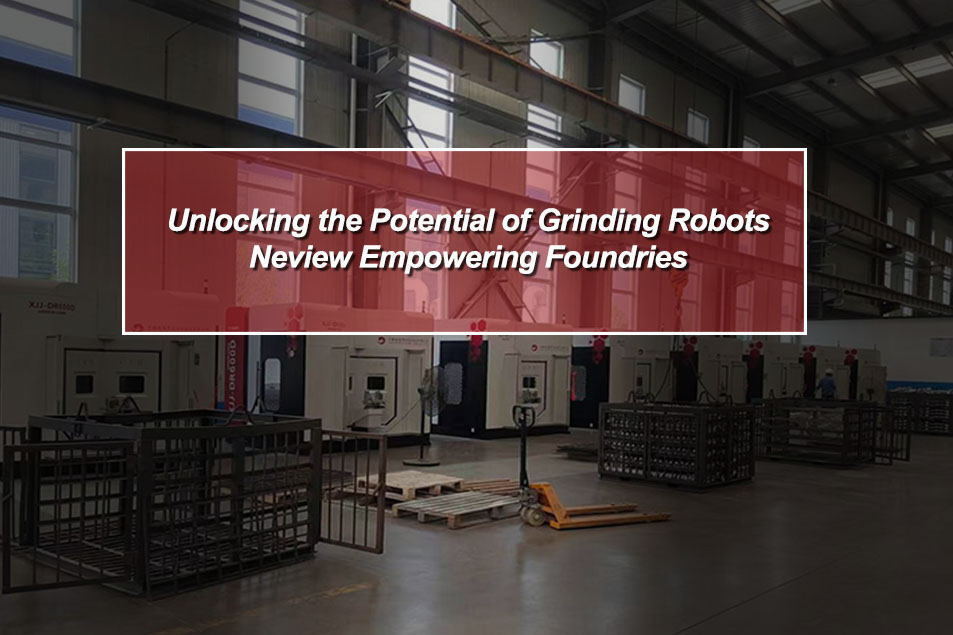
    Unlocking the Potential of Grinding Robots: Neview Empowering Foundries In the foundry industry, fully tapping the potential of grinding robots is crucial for enhancing the overall competitiveness of foundries. The Neview grinding robots provide strong support for foundries to achieve this goal through a series of advanced technologies and functions.   The eight - axis seven - linkage structure equipped in the Neview grinding robots is one of their core advantages. This complex and sophisticated structure enables the robots to move and operate freely in multiple dimensions, achieving precise grinding of various complex - shaped castings. Compared with traditional grinding equipment, it can complete grinding tasks more quickly and accurately, greatly improving grinding efficiency and quality. For example, when processing castings with irregular surfaces, the eight - axis seven - linkage structure allows the robots to easily fit the casting surface, ensuring that every part is evenly ground.   The intelligent compensation and flexible fitting technology is another key feature of the Neview grinding robots. For easily deformed castings, traditional grinding methods often cause damage to the castings. However, the Neview grinding robots can automatically adjust the grinding force and path according to the real - time state of the casting by intelligently controlling the current loop, position loop, and torque loop, achieving flexible grinding and effectively protecting the castings from damage. This technology not only increases the casting yield rate but also broadens the application scope of the robots in grinding castings of different materials and shapes.   The automatic error detection and compensation system is an important guarantee for the Neview grinding robots to ensure high - precision grinding. During the casting process, there may be small deviations in the size and shape of the castings, which will affect the grinding accuracy. This system uses high - precision displacement sensors to detect these deviations in real - time and automatically corrects the grinding path through background algorithms, ensuring that the robots can always grind according to an accurate trajectory, thus guaranteeing the stability and consistency of product quality.   In addition, the design of the Neview grinding robots focuses on seamless integration with the production processes of foundries. It can be customized according to the actual needs of foundries, and whether it is used for single - machine operation or integrated into an automated production line, it can exert its maximum efficiency, bringing efficient and stable grinding solutions to foundries.
    Read More
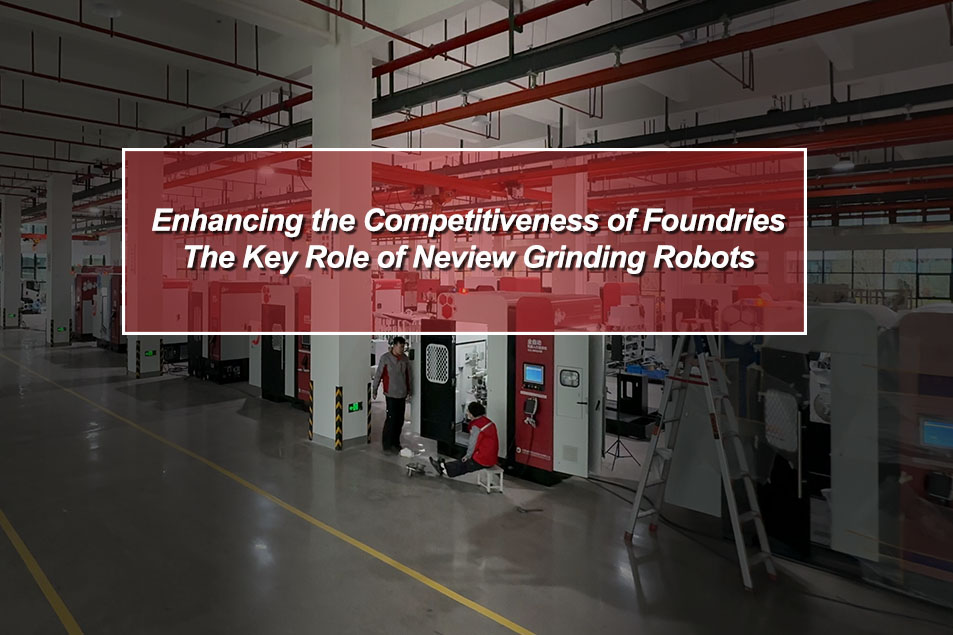
  • Enhancing the Competitiveness of Foundries: The Key Role of Neview Grinding Robots
    Enhancing the Competitiveness of Foundries: The Key Role of Neview Grinding Robots
    May 18, 2026
    Enhancing the Competitiveness of Foundries: The Key Role of Neview Grinding Robots In the increasingly competitive foundry industry, foundries face numerous challenges. How to improve production efficiency, ensure product quality, and reduce costs has become crucial. The grinding robots of Anhui Neview Automatic Technology Co., Ltd. provide comprehensive and efficient solutions for foundries.   The Neview grinding robots stand out with their unique eight - axis seven - linkage structure. This innovative design enables two - hand coordinated operation, greatly enhancing the flexibility and precision of the robots during the grinding process. Compared with traditional grinding methods, it can complete the grinding tasks of complex castings in a much shorter time, significantly improving production efficiency. For example, when processing large and complex castings, traditional methods may take several hours or even longer, while the Neview grinding robots can reduce the time to one - third or even less of the original time, thanks to their efficient operation mode.   In addition, the ultra - high rigidity and large load - bearing capacity of the Neview grinding robots enable them to easily meet the grinding needs of various heavy - duty castings. Taking the DR - 750B model as an example, both its workbench and robotic arm can bear a load of 200kg level, and it performs excellently in tasks such as the cutting and grinding of large riser stubs, ensuring the stability and continuity of the grinding work, and effectively avoiding grinding interruptions or quality problems caused by insufficient equipment load.   In terms of casting deburring, the Neview grinding robots also perform outstandingly. Their intelligent compensation and flexible fitting technology can automatically adjust the grinding force according to the material and shape of the casting by controlling the current loop, position loop, and torque loop, achieving fine deburring of easily deformed castings. At the same time, the automatic error detection and compensation system can detect and correct the casting errors in real - time, ensuring the accuracy and quality of deburring.   For foundries, the Neview grinding robots are not only powerful tools for improving production efficiency but also the key to enhancing product quality and market competitiveness. It helps foundries reduce labor costs while improving the stability and reliability of production, winning an edge for foundries in the fierce market competition.
    Read More
1 2
A total of 2 pages

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit
Contact Us: judy@ahxjj.cn

home

products

WhatsApp

Contact Us