Sep 10, 2026
Foundries Can’t Keep Grinders. What Work Can a Grinding Robot Actually Take?
The hardest shift to staff in a foundry is often not melting or molding. It is grinding.
Day shift can still be patched together. Night shift, hot weather, and year-end rush orders are when the finishing room empties first. The work is not optional. Unground gates, proud parting lines, and hole-edge burrs show up later in machining, assembly, and paint. The job is dirty, loud, and dusty. Numb hands and sore wrists are normal. When a skilled grinder leaves, you do not replace the “feel” in a week.
Most plants looking at grinding robots are not chasing a slogan. They are asking a simpler question: can this line still ship tomorrow.
What actually wears people out
From outside, grinding looks like an angle grinder on a casting. Anyone who has stood in the booth knows fatigue is only part of it.
The harder problem is inconsistency.
Castings from the same mold and the same heat do not arrive the same. Gate stubs vary in height. Flash is thick on one piece and thin on the next. Some parts are slightly warped. Some cavities will not accept a wheel. A skilled operator compensates by pressure, angle, and a couple of extra passes. A new hire under-grinds or knocks a datum face down. Piecework continues. Quality starts to drift.
Turnover makes it worse. Training a finisher takes time. Losing one experienced person takes cycle time and rework with them. Job ads can stay online. Castings will not wait.
Dust and labor rules are also pushing the job out of the plant. Iron dust, aluminum smear and noise, steel cutting load—none of that is solved by handing out earplugs. “Just hire two more people” is getting harder to use as a finishing strategy.
That is why automated grinding is entering foundries. Finishing has started to hold the whole line back.
Why casting grind is more awkward than machining
Machining starts from a blank that already has datums and tighter stock. Casting grind starts from something else.
Gate remnants can be high. Cutting force jumps immediately. Parting lines, vents, cold-shut edges, and ingates are irregular. The tool has to reach in without thinning the wall next to it. Sand castings and permanent-mold parts, iron and die-cast aluminum, do not leave the same burr. Die-cast flash can be thin and long. A sand-cast gate can be thick and hard.
Then there is casting variation. A millimeter or two on the same part number is not rare. A robot that only repeats one frozen path will grind air one day and cut into a rib the next. That is why a demo video can look clean and the same cell can disappoint on a real floor. Demo parts are usually better behaved than incoming work.
The hard part is not whether the arm can move. It is whether three things can hold at once:
the part can be located with acceptable repeatability; the path can move with the casting error; tooling and force can change by material and by feature.
Miss one, and the cell still runs. The quality does not.
What a robot can take—and what it should not
Start with the good fit.
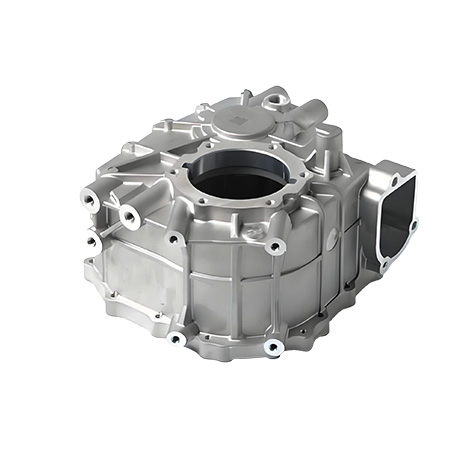
Stable volume, a short list of part numbers, and a grinding spec you can write down. Housings, brackets, valve bodies, wheel-type parts where the same gates, the same flash lines, and the same hole edges come back every day. That repetition is what a cell is built for.
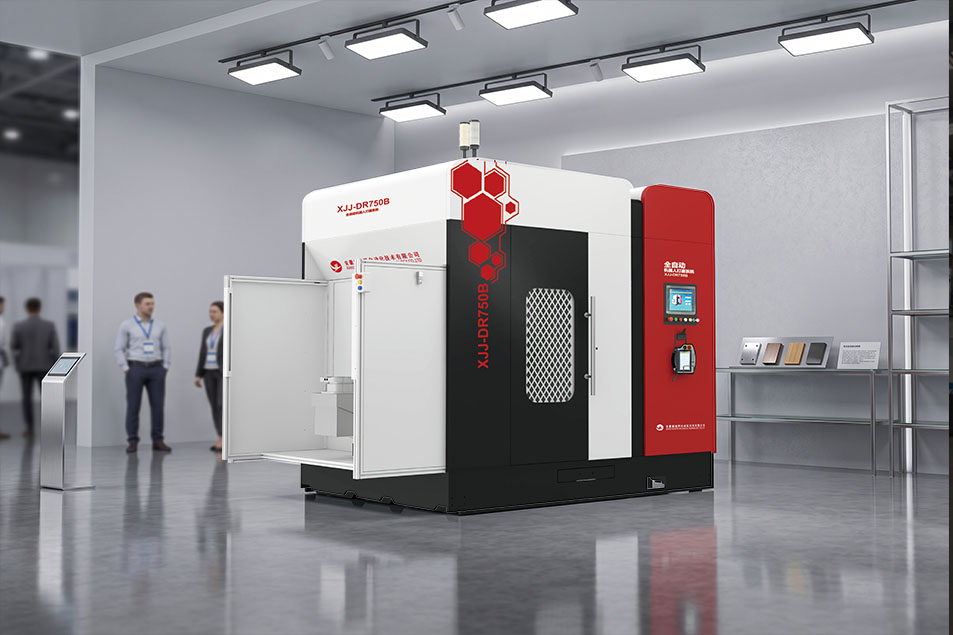
Dual stations exist for a practical reason: grind on one side, load on the other, so the machine is not waiting. For mid-volume small and medium iron or aluminum parts, that layout matches finishing better than a single fixture and a standing robot.
Heavy gates and thick flash are where people fade. Handheld tools lose force late in a shift and the cut goes uneven. A rigid, high-payload grinding unit is often steadier there. What matters on site is whether the table and arm can take the cutting force, and whether the enclosure actually contains dust and sparks—not how the machine photographs.
Now the poor first candidates.
Job shops with constant part-number changes will burn time on fixtures and teaching. If the casting may be revised before the clamp is finished, the cell becomes furniture. That is not “automation is impossible.” It means changeover rate and who owns the program have to be answered first.
Parts with almost no stable datum, or with very large piece-to-piece spread, also need caution. A dead path without measurement and compensation can create more rework than a person. Distortion-prone parts—thin aluminum walls, some covers—need force control, not more stiffness. If the machine cannot go light where it must go light, cosmetic faces ripple.
One more miss: grinding is only one slice of finishing. If cutting and shot blast are unstable, and sorting and transfer are still a crowd of people, one grinding booth just moves the bottleneck a meter downstream.
Iron, aluminum, steel, and mega die cast are not the same job
Cast iron: hard gates, heavy dust, fast wheel wear. The unit has to hold load, and dust collection cannot be decorative. Once iron volume is there, dual stations and dual spindles show up because waiting time is expensive.
Aluminum is different. It smears. Surfaces mark easily. Many aluminum jobs need flash gone and edges even, without wounding a datum. Tools change: disc cutters, mills, belts, brushes. An iron-grinding wheel strategy does not transfer. Thin walls need fine current, position, and torque loops. If those loops are crude, appearance parts show waves.
Steel asks for rigidity. The same gate size cuts harder than iron. If payload and table capacity are short, a pretty path still chatters.
Large integrated die-castings are another project type. Big envelopes, long flash, many surfaces, and a takt set by the die-cast cell. Scaling a standard booth is not the work. Floor space, handoff from the casting island, and fixture strategy decide the project.
You do not buy “a robot.” You buy a finishing method for a material, a geometry, a volume, and a process.
What plants usually underestimate
Fixtures. Simple nests are fast and cheap, and they move. Self-clamping nests are stable and slow to build. Some machines add a press-down axis to drop some cylinder modules and cover more part numbers. “The robot has a camera, just dump the parts” is still rare on real foundry floors. Vision and auto-locate, when they are used, are there to cut hard locators and cut reteaching—not to delete fixturing.
Consumables and process. Wheels, burrs, discs, flap wheels, rotary files for iron and steel; a different set for aluminum. The wrong tool on the right machine still makes scrap. A cell does not arrive knowing which cutter belongs on which feature.
Incoming consistency. Mold upkeep, pouring stability, and how the gate was cut before grind all land on the program. Compensation can swallow some size scatter. It cannot swallow a process that is not under control. Before automation, tighten gate location and flash condition. Do not ask the cell to eat every upstream swing.
Ownership. Someone has to own programs, changeovers, wheel changes, and compensation values. A supplier cannot live in the plant forever. If nobody on the floor will touch the teach pendant, a good start-up decays in a few months.
Four questions before you buy
Will these part numbers still run in six months? Is there enough daily volume to feed a full shift? Can process engineering mark the gates, the flash, and the faces that must not be touched? Is there a person who will own fixtures and programs?
If two of those are blank, do not start with “lights-out.” Start with the dirtiest, heaviest, most repetitive features. Lock takt and quality. Then decide whether bin picking, infeed conveyors, or sorting belong in the next step.
For foundries and die-casters that already have stable volume, the value is usually plain: quality that does not collapse when a skilled grinder quits; finishing that can still run on night shift; fewer dust and labor fights; the same part number finished to the same standard, regardless of who is on the wheel that day.
Companies that live in casting finishing—Neview is one of them—are judged on whether compensation tracks casting scatter, whether a heavy gate can be cut, whether aluminum can be worked lightly, whether iron and steel can be held, and whether the grind cell can connect to handling later. Those points only mean something against a real part and a real volume.
Automated grinding will not clean up an entire foundry. It is good at the work that repeats every day, can be specified, and has already worn people down.
The shop-floor test is still the same: when the skilled hand is gone, does the part still come out the same.
Read More



 IPv6 network supported